Case Study

Major Material Handling OEM – Austria, Spain, UK

  • Client: Major material handling OEM – Austria, Spain, UK
  • Industry: Warehousing, distribution, and material handling
  • Location: Leicester, UK
  • Services provided: Control system upgrade for conveyor-based material handling line, safety upgrade, vision and barcode integration
  • Software used: AutoCAD (mechanical design review), Eplan Electric P8, Siemens TIA Portal
  • Hardware used: Siemens S7-1500 PLC, ET200S remote I/O, Siemens TP1200 Comfort HMIs, Keyence imaging system, barcode printers and scanners, safety light curtains, ifm Sensos, SEW Drives
  • Key result: Standardized, scalable control platform for multiple conveyors, diverters, sorters, lifters, and inspection stations with improved visibility and safety
  • Duration: 14 months - including design, programming, and commissioning
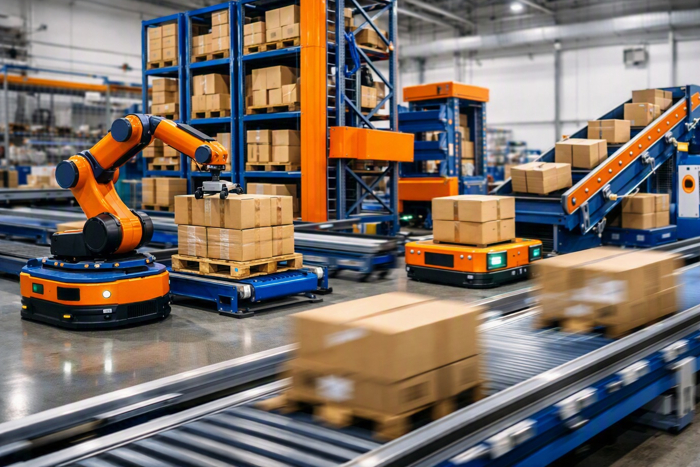
Material Handling Project

Client & Project Background

The client operates a high-throughput material handling unit with multiple master and slave conveyor lines, diverters, sorters, lifters, barcode printers, and scanners for carton and tote movement. They wanted to upgrade their control system to a modern Siemens S7-1500 platform, improve diagnostics and safety, and integrate imaging-based inspection without disrupting ongoing operations. APC Engineering Services was engaged to deliver a complete control upgrade, from electrical design and network architecture to PLC/HMI programming and field integration.

Challenge / Requirements

  • Existing controls were fragmented, with mixed hardware and limited diagnostics, making fault finding and maintenance time-consuming.
  • Material flow involved several coordinated devices: master and slave conveyors, diverters, sorters, vertical lifters, barcode printers and scanners, and new Keyence imaging-based inspection.
  • The client required a unified PLC and HMI platform with clear I/O structure, PROFINET network configuration, and safe stopping zones using light curtains.
  • Any upgrade had to be carried out with minimal production downtime and allow future expansion of new conveyor sections or stations.

Solution (APC approach)

1. Design & Engineering

  • Reviewed the mechanical layouts and conveyor arrangement using AutoCAD drawings to validate sensor/actuator placement and cable routing before finalizing the control design.
  • Developed detailed electrical schematics in Eplan Electric P8, including power distribution, control circuits, I/O channel allocation, network topology, and safety wiring (light curtains and e-stops).
  • Structured the system into functional zones (infeed, main sorter, lifters, inspection, outfeed) to keep documentation and troubleshooting logical for maintenance teams.

2. PLC, I/O, and Network

  • Selected Siemens S7-1500 as the central controller and ET200S remote I/O stations for field-level connectivity, ensuring scalable and modular control panels.
  • Used Siemens TIA Portal to design the complete I/O structure, PROFINET network configuration, and tag-based program organization for each conveyor, diverter, sorter, lifter, and safety device.
  • Standardized software blocks for typical conveyor segments and devices so future extensions can be engineered faster with tested logic.

3. HMI and Operator Interface

  • Designed multiple operator control stations using Siemens TP1200 Comfort panels, providing local control, status pages, and alarm diagnostics for each major zone.
  • Implemented clear mimic screens showing conveyor states, jam points, inspection results, barcode read status, and safety zone conditions.

4. Inspection, Barcode, and Safety Integration

  • Integrated a Keyence imaging system for inline inspection, exchanging pass/fail and measurement data with the PLC to trigger sorting or rejection.
  • Interfaced barcode printers and scanners for product identification and routing decisions, with PLC-managed verification and error handling.
  • Added and wired safety light curtains to create safe access zones, ensuring controlled stopping and restart logic in coordination with S7-1500 safety routines.

Results & Benefits

  • Achieved a unified, Siemens-based control architecture that simplifies maintenance and provides a clear expansion path for additional conveyors and stations.
  • Improved fault diagnostics and reduced troubleshooting time through structured I/O, standardized function blocks, and detailed TP1200 Comfort HMI alarm and status screens.
  • Enhanced product quality and traceability with integrated Keyence inspection and barcode systems, enabling automatic rejection and routing based on inspection and read results.
  • Increased safety and compliance by adding light curtains and clearly defined safety zones, allowing maintenance access while protecting operators and equipment.

Tools & Technologies Used

  • Design: AutoCAD for mechanical layout review, Eplan Electric P8 for electrical schematics, panel layouts, and device lists.
  • PLC & HMI: Siemens S7-1500 CPU, ET200S remote I/O stations, TIA Portal for PLC programming, I/O structuring, PROFINET configuration, and TP1200 Comfort HMI application development.
  • Inspection & identification: Keyence imaging system for inline visual inspection; barcode printers and scanners for automatic identification and routing.
  • Safety: Safety light curtains and emergency stop circuits integrated into the S7-1500-based safety and interlock logic.

“By upgrading our material handling control system to a Siemens S7-1500 platform with ET200S remote I/O, APC Engineering Services has given us a stable and future-ready solution. The new TP1200 Comfort HMIs, integrated Keyence inspection, and barcode systems have greatly improved visibility on the line and reduced downtime. Their structured approach to safety and diagnostics has made day-to-day operation and maintenance far more efficient.”

Client Testimonial